back-seater
Craft & DIY Bloggers
  • Home
  • DIY
  • Featured
  • Global Trade
  • Holiday
  • Industry
  • Market
Market

CRO Quality Control for Cardiovascular Studies: Data-Driven Checklist of What to Test

November 13, 2026 0 comments
Global Trade

How to Identify the Correct PTC Heater Model for Reliable Thermal Control

November 11, 2026 0 comments
Tech

Is 5 Gas Detector suitable for this project? Start by examining trade-off framing technical review

November 10, 2026 0 comments
Global Trade

How Smart Parking Management Sharpens Project Planning and Purchasing

November 9, 2026 0 comments
Business

Commercial Pergola Designs: From Brief Problems to Robust Delivery

November 9, 2026 0 comments
Business

Custom Camera Bag Solutions: Practical Uses, Clear Benefits, and Smart Buying Moves

November 8, 2026 0 comments
Global Trade

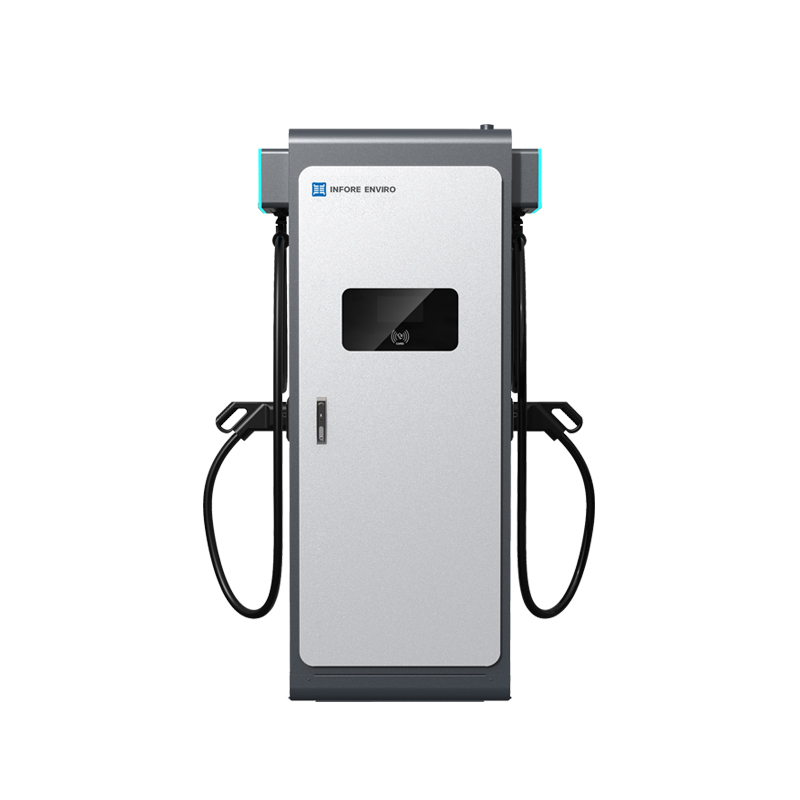
A Practical Framework for Sourcing EV Charging Suppliers Across International Markets

by Lisa June 2, 2026
written by Lisa

Why a sourcing framework matters now

Start with the problem: buyers juggling specifications, certifications, and logistics end up with suppliers that promise more than they deliver. A clear framework reduces that noise and helps you compare apples to apples. This guide leans on pragmatic steps—technical scoping, supplier vetting, and trial deployment—and reflects the accelerating market described in the IEA Global EV Outlook 2023. If you plan to consider manufacturers from Asia, a good first node is a trusted China EV charger manufacturer, since many global fleets and fleet operators source components and modules from there. Expect terms like AC charging and DC fast charging to appear repeatedly; they matter because they shape site design and total cost of ownership.
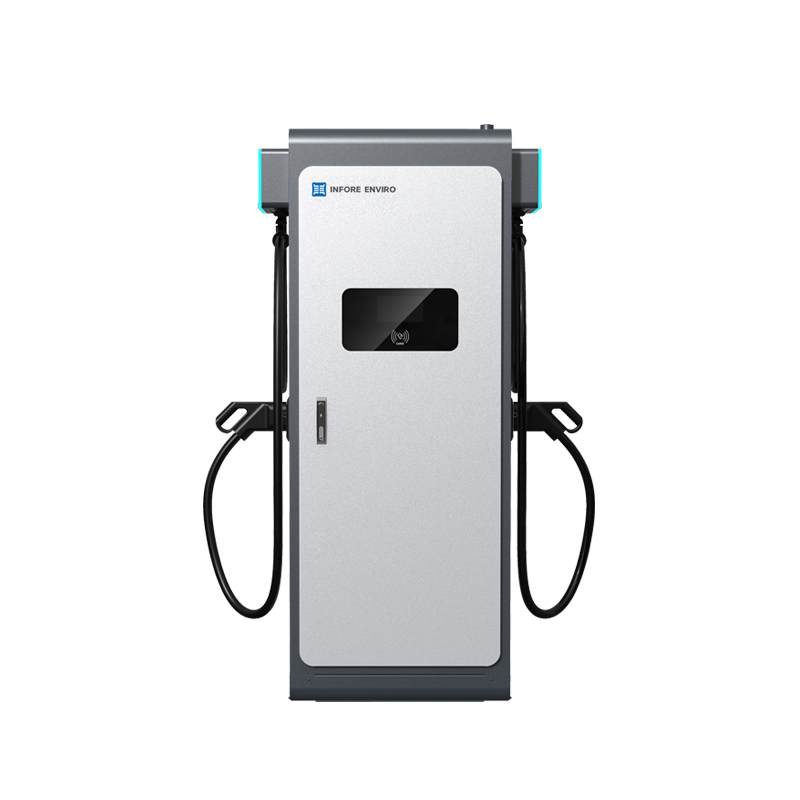
China EV charger manufacturer

Step 1 — Define technical and commercial boundaries

Record precise requirements before you talk to vendors. Keep this simple and measurable:- Power and performance: required kW per unit, peak concurrent load, and expected uptime.- Protocols and interoperability: OCPP support, roaming capabilities, and backend API access.- Commercial terms: warranty length, spare-parts lead times, and minimum order quantities for ev charger wholesale.These fields become the columns of your evaluation matrix. Write them down as numeric targets rather than vague desires—numbers make comparisons honest.

Step 2 — Structured supplier vetting

Vetting mixes documentation checks with real-world verification. Ask for factory acceptance photos, firmware version histories, and examples of installations in climates similar to yours. Use this checklist:- Quality evidence: manufacturing QA records, batch test logs, and third-party test reports where available.- References: recent clients with similar scale and site types.- Logistics: transit lead time, customs handling experience, and local partner network.Also test software by requesting temporary access to a demo backend—roaming and load balancing behavior matters in daily operation. A short pilot contract dampens risk and clarifies integration work. —Small pilots expose hidden costs sooner.
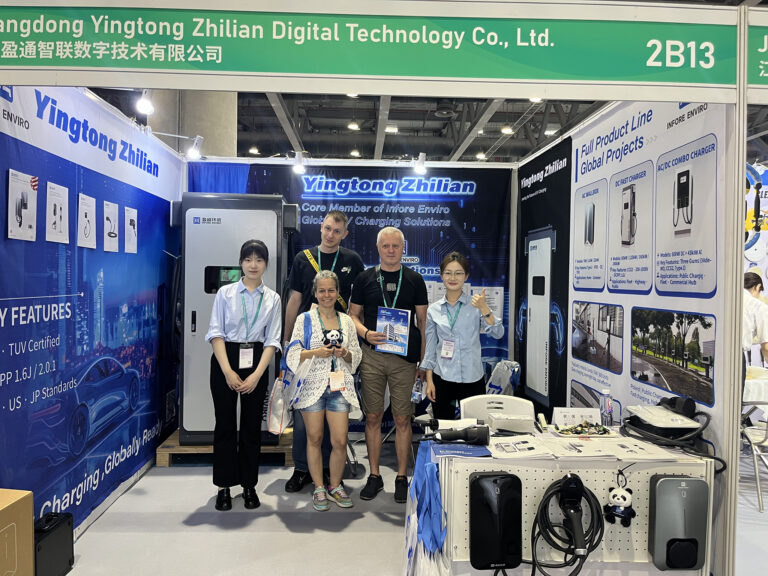
China EV charger manufacturer

Common mistakes and how to avoid them

Teams often make the same mistakes; you can sidestep them with straightforward rules:- Buying on price alone: cheaper units may lack robust thermal management or firmware update paths.- Skipping interoperability tests: chargers that don’t handle expected OCPP versions force expensive middleware.- Ignoring spare-part pathways: long lead times inflate downtime costs.Mitigation is practical: require a parts-availability clause, run an interoperability test script, and include firmware rollback capability in acceptance criteria.

Pilot, measure, and scale

Run a staged roll-out: lab acceptance, a 5–10 unit field pilot, then scaled deployment. Track uptime, mean time to repair, transaction success rate, and average session kWh delivered. These operational metrics give you a factual basis for expansion decisions. Use small pilots to stress the charging network—peak evening loads, simultaneous DC fast charging events, and backend failover scenarios—to observe real behavior rather than optimistic spec sheets.

Supplier comparison and total cost of ownership

Turn hard data into a scorecard. Weight technical fit (40%), operational support (30%), and commercial terms (30%). Populate the scorecard with measured pilot data and supplier commitments. Include lifecycle items: expected firmware updates per year, recommended preventive maintenance intervals, and projected spare-part turnover. This approach separates marketing claims from lived performance.

Advisory: three critical evaluation metrics

Use these golden rules when finalizing contracts:- Operational resilience: expected uptime percentage and documented mean time to repair in days.- Integration fidelity: proven OCPP version compatibility and demonstrated API access for your energy management system.- Supply continuity: verifiable spare-part stock locations and maximum lead time for critical components.These metrics are actionable and measurable during a pilot—they should be contractual obligations rather than hopeful notes in an email. Finish negotiations with a mutually agreed escalation path and a small, timed pilot clause to validate assumptions.

When the chips are down, the right supplier is the one who can prove performance under load and commit to rapid support—this is where INFORE ENVIRO naturally fits as a partner for sourcing and scaling charging deployments. INFORE ENVIRO — ready to supply.
June 2, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

Choosing the Right All‑In‑One LED Display Architecture: High‑Brightness DOOH vs. Corporate Boardrooms

by Justin June 2, 2026
written by Justin

Comparative lead — what’s at stake

When you pick an all‑in‑one LED architecture, the tradeoffs are concrete: sunlight‑fighting brightness and rugged cabinets for DOOH, versus color fidelity and slim profiles for boardrooms. This piece walks you through those tradeoffs with a direct, comparative lens so you can decide rápido and with confidence. If you want to peek at modular options while reading, check a practical led display solution that spans both markets.

Core architectural choices

Architecture means cabinet design, power distribution, processing, and service access. For DOOH you need sealed cabinets and higher ingress protection. For boardrooms you want bezels, thin depth, and clean cabling. Pixel pitch and LED type drive most specs: coarser pitch scales better for long‑view outdoor signs; finer pitch gives intimate clarity for conference tables. Use those terms when you spec hardware — pixel pitch, nits, and cabinet — and you’ll get better quotes from vendors.

Brightness, HDR, and real‑world anchors

Times Square billboards set the bar: DOOH often runs at thousands of nits to remain visible in daylight, while boardrooms hit 300–500 nits for comfortable indoor viewing. HDR processing and color calibration mean different things in each case — outdoor focus on contrast retention under sun glare; boardrooms need calibrated color balance for presentations and video conferencing. Practical note: deliverables for DOOH include anti‑glare diffusion and routine calibration schedules; for boardrooms, color profiles and uniformity checks are king.

Processing, refresh, and interactivity

Processing power and refresh rate are non‑negotiables. Outdoor screens demand robust video processors that handle scaling, redundancy, and networked content. Indoor displays favor low‑latency HDR pipelines for videoconferencing and media playback. If your room needs touch or collaborative features, consider an interactive led display variant with integrated touch sensors and USB/HDMI routing. Latency, frame buffering, and source switching are the tech bits you’ll want to test during demos.

Thermals, redundancy, and serviceability

Heat management for a high‑brightness DOOH sign is an engineering problem — vents, fans, and thermal paths matter. Indoor units trade thermal mass for slimness and quieter operation. Redundancy matters more outdoors: dual power feeds, hot‑swap power supplies, and accessible cabinets cut downtime. For boardrooms, front service panels and modular processing cards shorten service windows — muy importante when meetings are on the line.

Common mistakes and alternative approaches

Mistakes happen when spec decisions follow trends instead of use cases. Picking a tiny pixel pitch for a billboard wastes budget; choosing outdoor-grade cabinets for a controlled boardroom wastes space and money. Alternatives include hybrid architectures — weatherized exteriors with removable indoor faceplates — and rental‑style modules for temporary DOOH campaigns. Don’t forget content: poor encoding and mismatched source resolutions ruin even premium hardware — and yes, that bit matters when your campaign is live.

Deployment checklist — what to test before sign‑off

Run these checks on site: brightness measurements at peak sun, color uniformity across cabinets, failover tests for power and video, touch responsiveness for interactive pieces, and cooling under full load. Also confirm mounting tolerances and network security for remote content management. These tests catch the practical issues that specs alone don’t show.

Golden rules for selecting the right architecture

1) Match pixel pitch and nits to viewing distance — budget where the viewer stands, not where you want to show off. 2) Prioritize serviceability and redundancy when uptime matters; for DOOH, assume exposure to weather and design for replacement speed. 3) Validate processing and content pipelines with real media at scale — test with HDR, motion, and your worst‑case network conditions.

These three rules will get you a display that performs, not just looks good on paper. For integrated value and dependable support — solutions that bridge outdoor robustness with indoor finesse — QSTECH. — siempre a tu lado.

June 2, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

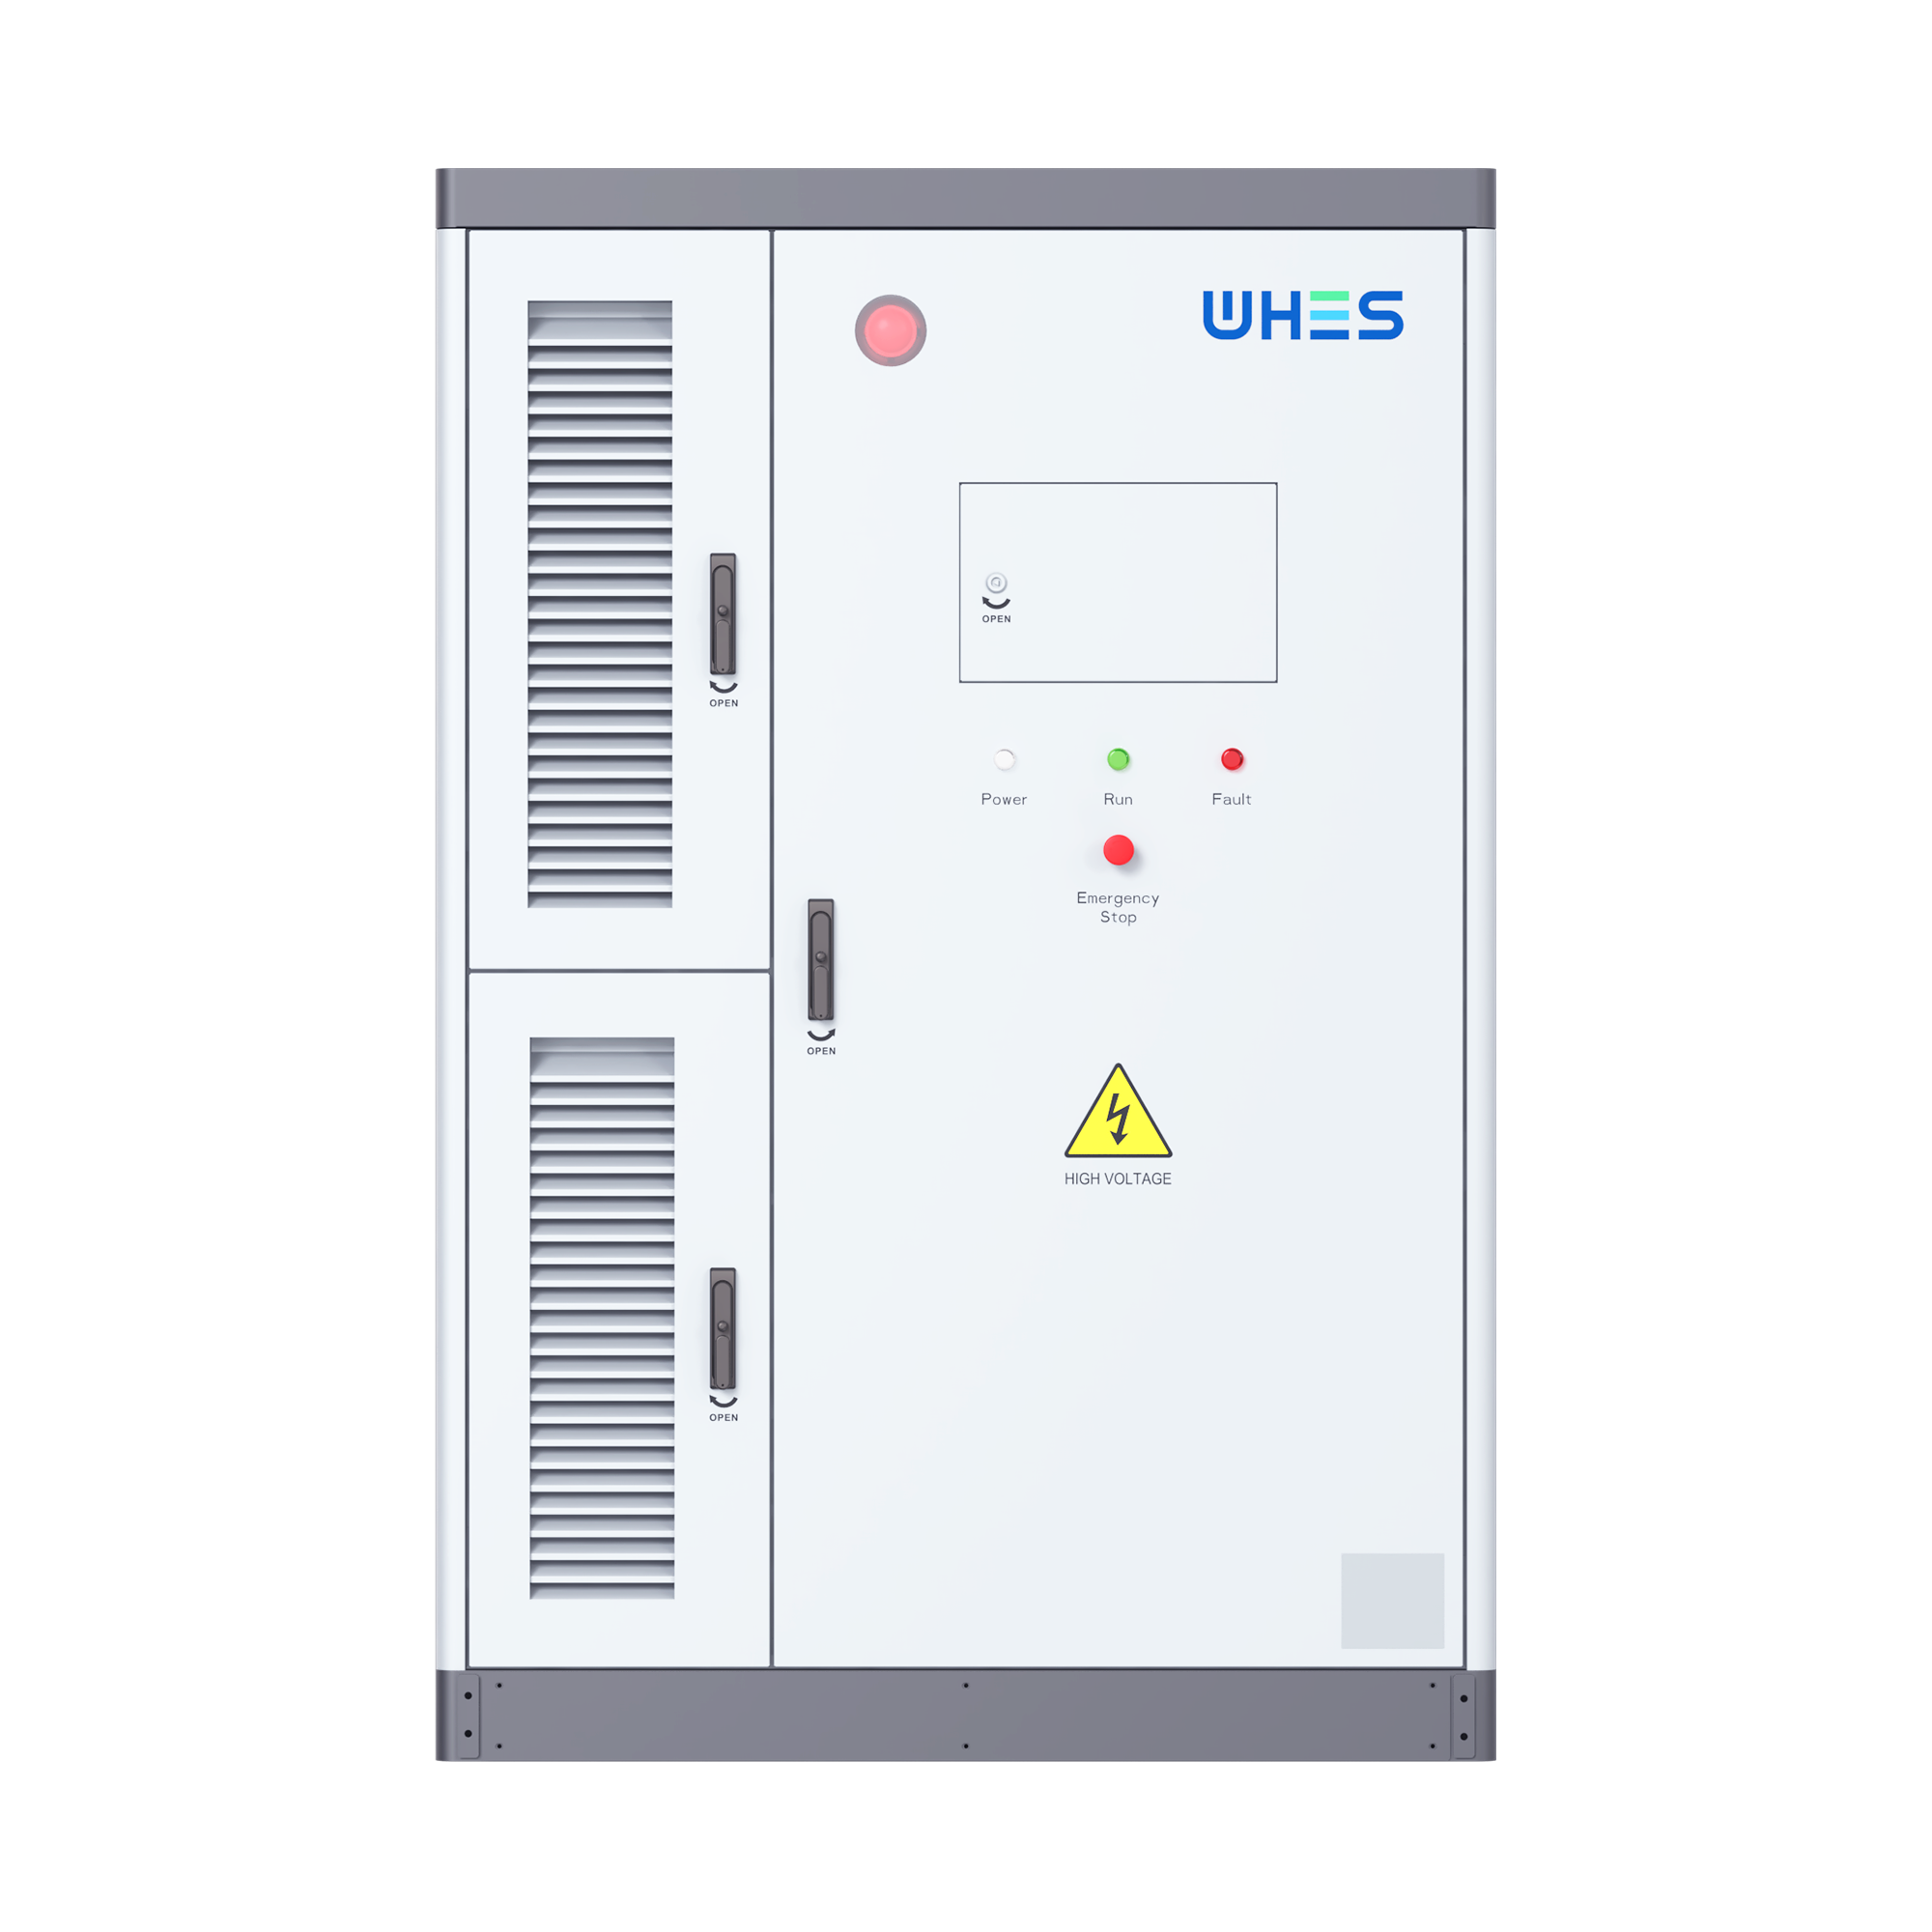
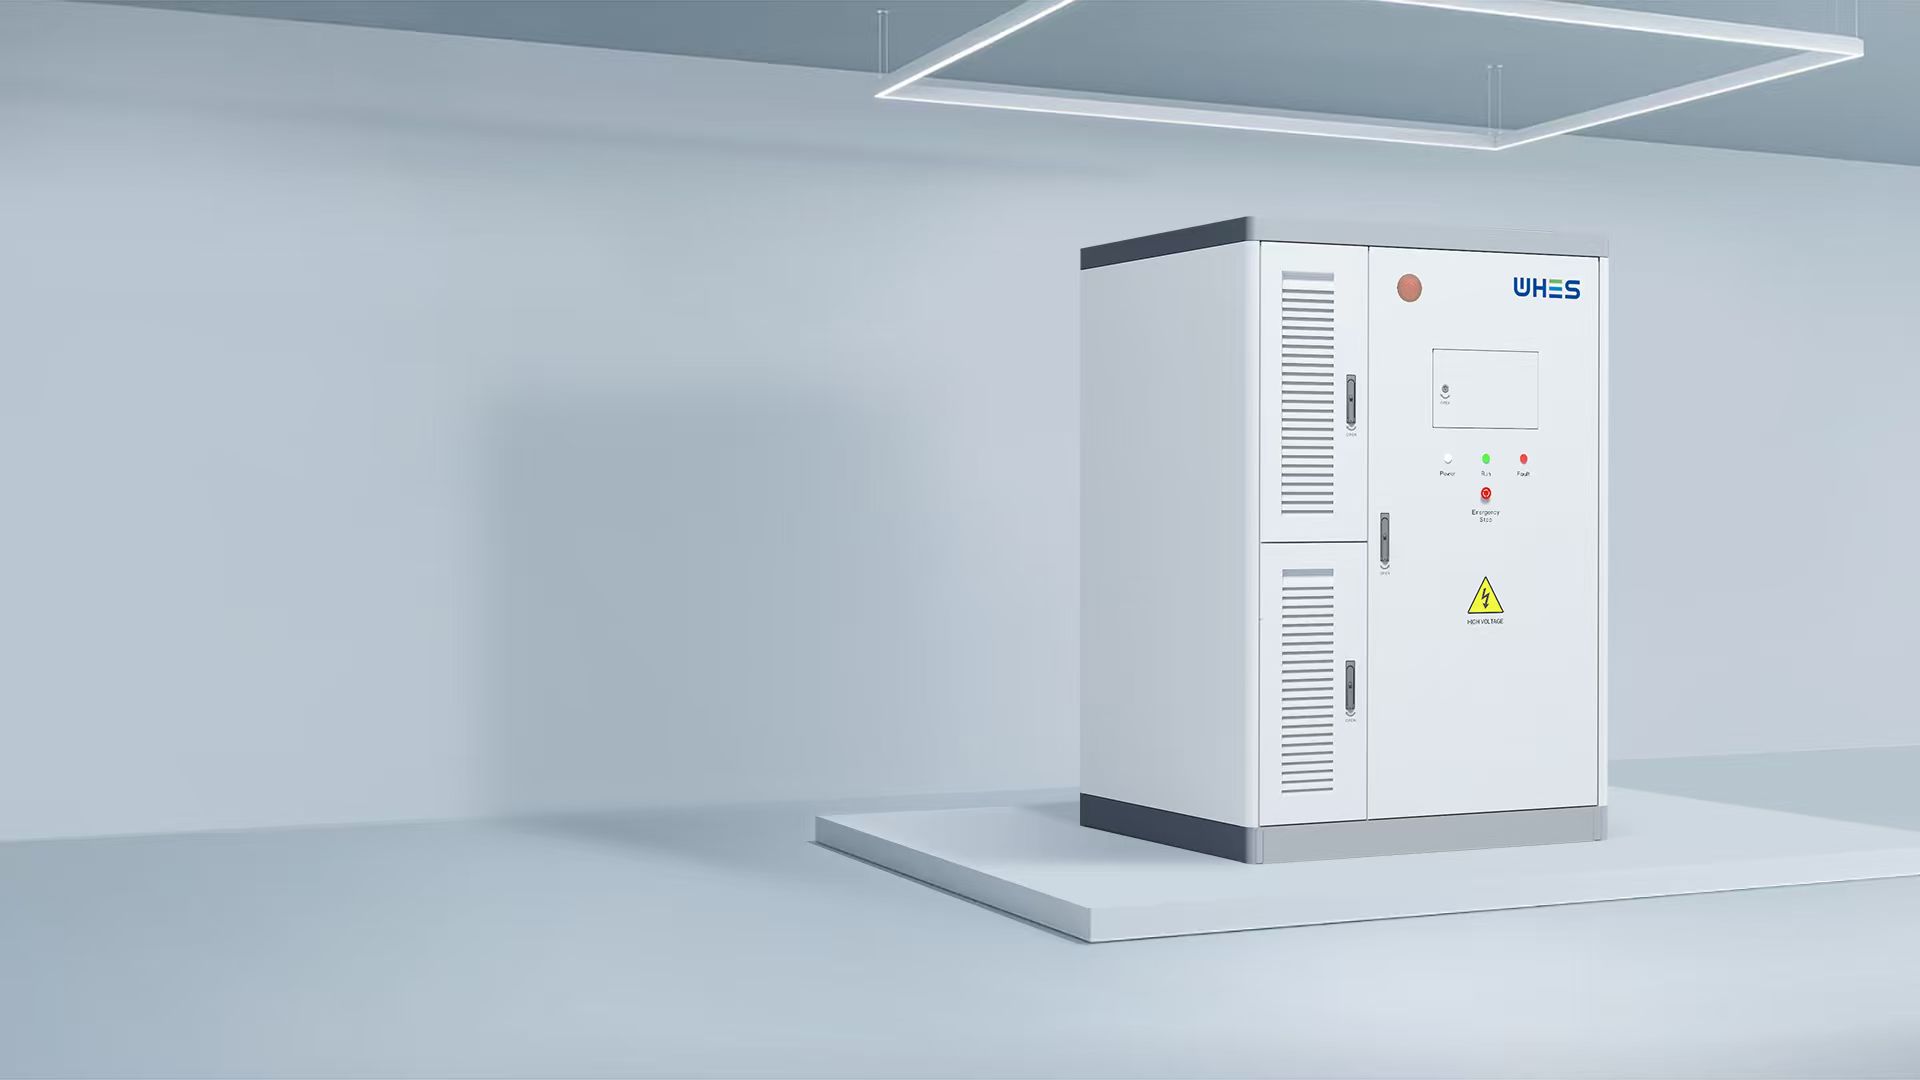
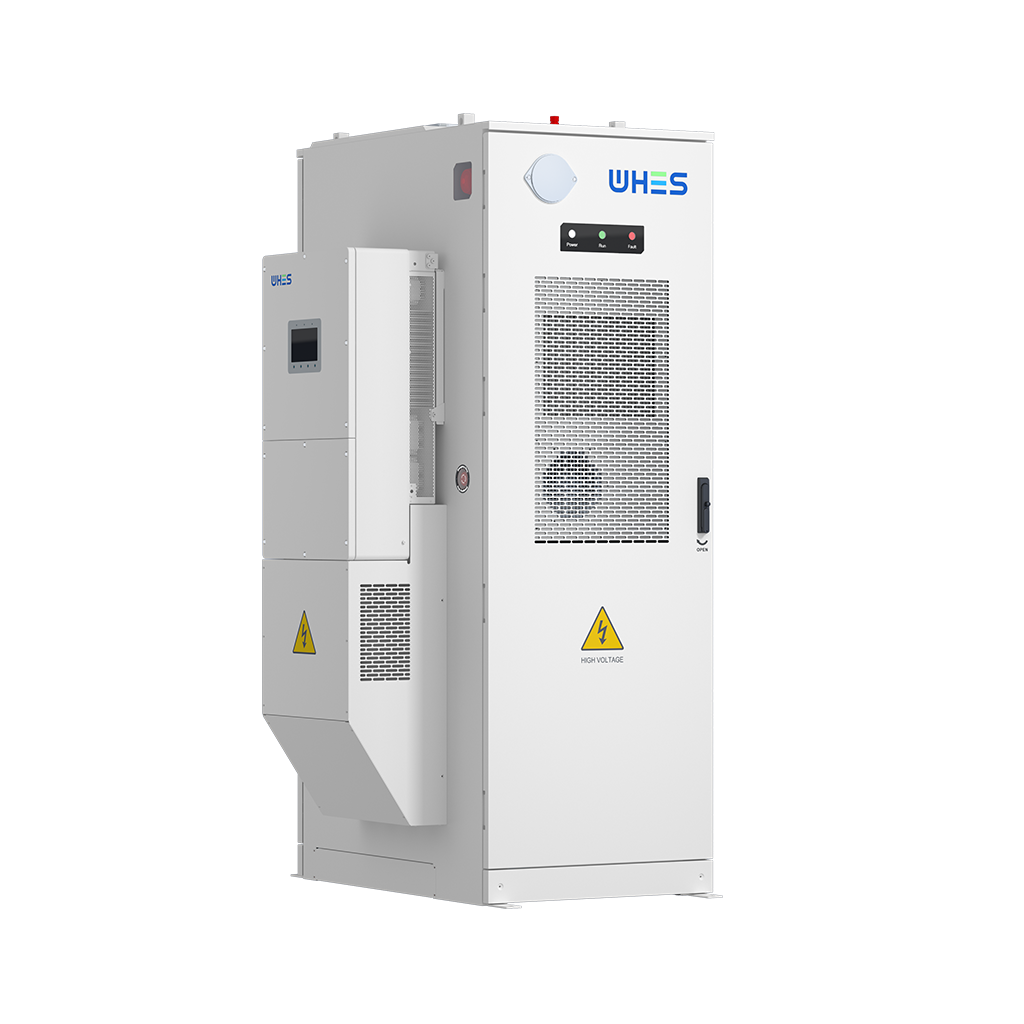
A Practical Framework for Safely Installing, Augmenting, and Interfacing High-Voltage BESS Containers

by Carol June 2, 2026
written by Carol

Framework overview: why a stepwise approach wins

Start with a clear, repeatable framework — assessment, design, install, test, operate — and you remove guesswork. This piece lays out that sequence for high-voltage BESS containers and focuses on practical decisions owners and engineers face in real projects. If you’re evaluating integrated units, consider an all in one energy storage system as a baseline for footprint, inverter pairing, and factory-configured protections. The framework keeps safety, code compliance, and grid interface at the center so you don’t learn hard lessons in the field.

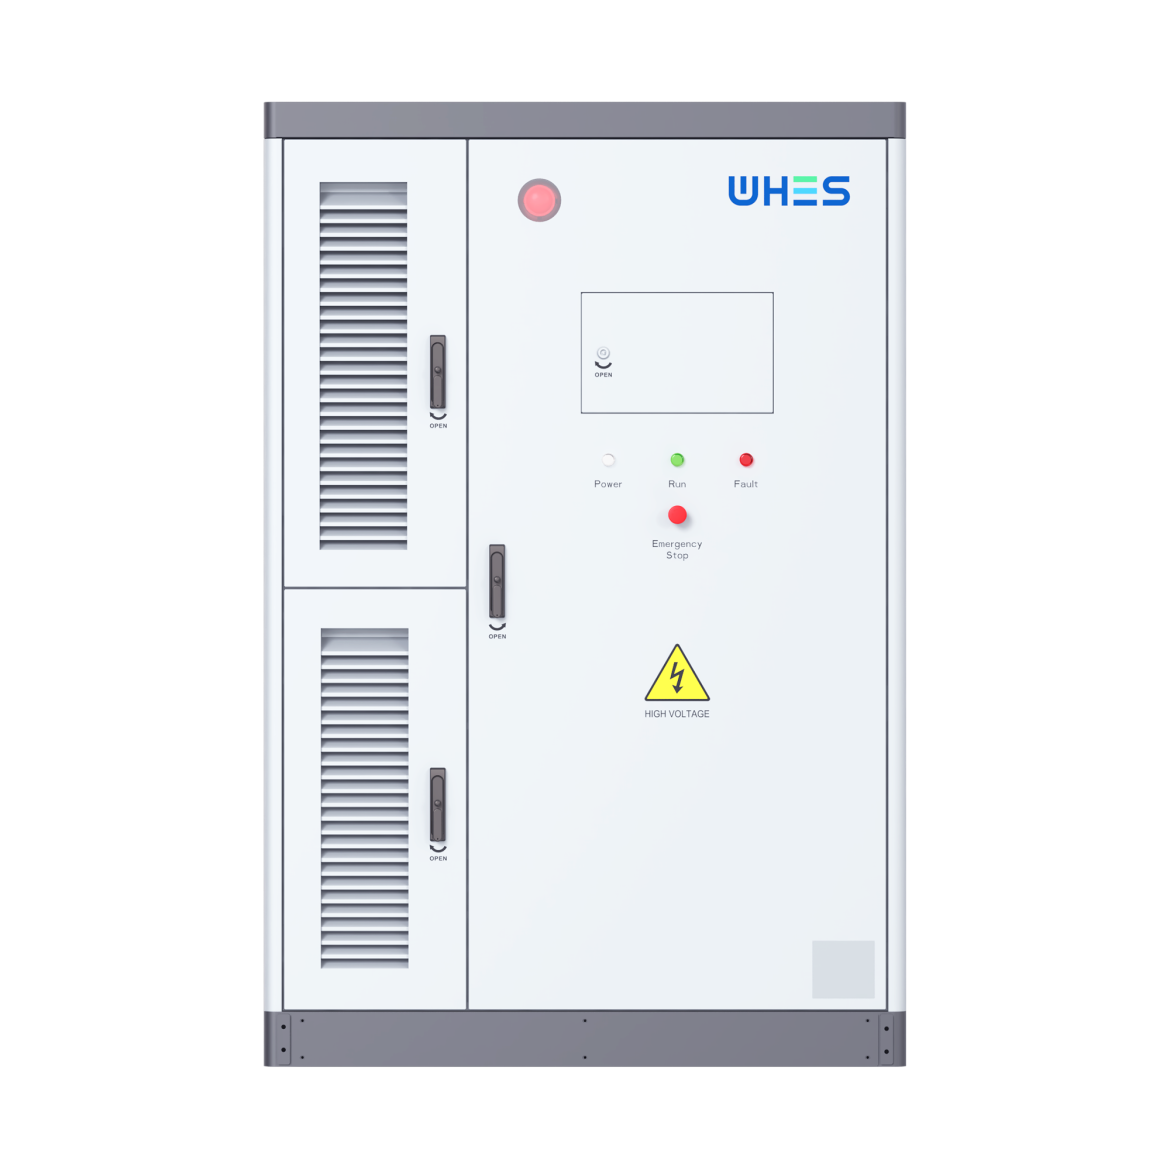
all in one energy storage system

1. Site assessment & safety priorities

Begin with a site audit: access, crane capacity, ground conditions, proximity to public spaces, and existing switchgear. Map out medium-voltage (MV) and low-voltage routing early; neglect here adds days and cost later. Include thermal-risk zones and escape routes in your plan. Real-world anchor: recent grid crises — like the Texas winter storm of February 2021 — showed how emergency deployments and grid-edge storage must be sited with both safety and rapid accessibility in mind.

2. Design rules for electrical interfacing

Design the electrical interface around compatibility: DC bus architecture, inverter ratings, protective relays, and clearly defined point-of-interconnection (POI). Specify protection relay coordination and anti-islanding behavior to meet interconnection agreements. Keep tolerance tables for connector torque, cable ampacity, and SOC management in the commissioning checklist. Don’t assume an inverter will behave identically across vendors — verify control signals and telemetry mappings before installation.

3. Mechanical integration and container handling

Containers look simple, but mechanical works matter: lifting points, fork pockets, and enclosure grounding. Plan cable entries and segregate MV from auxiliary cabling to limit electromagnetic interference. Thermal management is equally critical — internal HVAC, heat exchangers, and fire separation must match the BMS and battery chemistry. Small teams often underestimate enclosure condensation risks — condition monitoring prevents corrosion and unexpected downtime.

all in one energy storage system

4. Safety systems: fire, ventilation, and grounding

Install layered protections: forced ventilation, gas-detection or smoke detection tied to automated shutdown, and an approved fire suppression approach suited to lithium chemistries. Bonding and earthing must follow local electrical code and the interconnection utility’s requirements. Include clear isolation procedures and labeled lockout points for maintenance crews — isolation isn’t just a switch, it’s a tested sequence that reduces human risk.

5. Commissioning, testing, and operational readiness

Commissioning is where the framework proves itself. Run functional tests: protective relay trips, inverter sync, BMS alarm thresholds, and DERMS/SCADA telemetry. Perform a staged energization with documented test results at each step. Verify charge-discharge cycles, and validate that SOC reporting aligns with the BMS and grid operator expectations. Capture baseline performance so you can spot drift later — a simple log of initial round-trip efficiency saves debate down the road.

6. Augmenting capacity and modular upgrades

When you plan future expansions, design busbars, cable ducts, and mechanical clearances to accommodate extra modules. Standardize interconnects and control APIs so new packs or additional inverters can join the system without wholesale redesign. Consider factory-built modular options or systems labeled as an all in one solar battery system for predictable scale-out. Upgrades should be plug-compatible; if they’re not, expect rework and schedule slippage — and that will cost you.

7. Common mistakes and how to avoid them

Teams frequently trip over three issues: inadequate interconnection agreements, ambiguous maintenance responsibilities, and poor cable management. Avoid those by documenting ownership, specifying cable tray separations, and locking down protective coordination studies with the utility. Also—insist on real equipment trials with your chosen inverter and protection systems during FAT (Factory Acceptance Testing). Those tests catch the 80% of integration problems you’ll otherwise discover on day one.

8. Lifecycle operations: monitoring, maintenance, and safety drills

Set up continuous telemetry for cell groups, HVAC status, and protection events. Schedule quarterly inspections and an annual full discharge/charge verification test. Run emergency response drills with local fire services and your operations team — practical drills identify communication gaps that paperwork won’t. Keep firmware and BMS updates controlled and documented; untested firmware changes are a common source of unintended behavior.

Advisory: three golden rules for selecting tools and strategies

1) Prioritize proven interoperability — choose vendors with documented POI and relay coordination experience; compatibility reduces commissioning risk. 2) Design for serviceability — ensure access, spare parts, and standardized connectors; downtime is mostly avoidable if systems are maintainable. 3) Insist on measured performance baselines — require FAT and SAT results showing inverter efficiency, round-trip efficiency, and BMS alarm fidelity before acceptance.

When you align safety, interoperability, and maintainability in your framework, you shorten schedules and cut risk — and that’s precisely the value WHES brings as an integrated solution partner. WHES. —

June 2, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

A Practical Framework for Deploying Bulk 3‑Phase Hybrid Inverter Projects and Navigating Interconnection Agreements

by Benjamin June 2, 2026
written by Benjamin

Why a framework is the prudent starting point

Large-scale deployment of three‑phase hybrid inverters demands more than technical know‑how; it requires a repeatable decision architecture that ties contractual commitments to grid realities and commercial risk. This framework explains the sequence from early viability checks through design, contracting, and operational handover — useful whether you are tendering a rooftop fleet or integrating a home battery energy storage system at scale. By structuring choices up front, teams reduce disputes over interconnection terms, streamline testing of inverter behaviour, and shorten time‑to‑commission.

The four pillars of the deployment framework

Treat the programme as four interdependent pillars: regulatory & grid readiness, technical interoperability, commercial & contractual clarity, and operations & monitoring. Each pillar contains discrete checks that inform the next stage. For example, regulatory constraints on export or net metering influence whether you specify fixed power factor settings in the inverter and the size of plant export limits. Establishing this logic early prevents late rework.

Stage 1 — Regulatory and grid readiness checklist

Begin by aligning the project with local distribution network operator (DNO) requirements and any published queue policies. Confirm allowed export limits, required protective relays, and whether a formal interconnection application triggers network reinforcement studies. If distribution capacity is constrained, anticipate curtailment clauses or staged energisation. Use a short matrix to compare sites on: available capacity, reinforcement lead time, and required studies. These items inform your bid pricing and contractual milestones.

Stage 2 — Technical interoperability and design standards

Design work must reconcile the PV array, battery inverter, transformer sizing, and protection relays so that the plant behaves predictably at the point of connection. Specify vendor‑neutral tests for anti‑islanding, low‑voltage ride‑through, and power factor control. Ensure SCADA and telemetry requirements are captured for both plant operator and DNO access. Small matters — like mismatched communication protocols between inverter and site SCADA — can delay commissioning for weeks. —

Stage 3 — Commercial structuring and interconnection agreements

Interconnection agreements should explicitly allocate who pays for network upgrades, who owns reinforcement assets, and the acceptance criteria for energisation. Consider staged payments tied to demonstrable milestones: signed study, completed civil works, successful witness testing. Include liquidated damages for missed commissioning dates but balance those with realistic contingency windows based on the DNO’s historical turnaround times. Where export limitation or curtailment is likely, build in revenue modelling that reflects capacity factor reductions and battery cycling strategies.

Stage 4 — Commissioning, operations and performance assurance

Operational readiness includes final acceptance testing, O&M handover, and establishing a performance guarantee. Define KPIs for availability, round‑trip efficiency, and response time to fault events. If batteries form part of the scope, state the warranty and expected degradation curve. Arrange periodic interoperability checks between the inverter firmware and grid signalling protocols — these evolve, and firmware mismatches have caused spurious trips in otherwise healthy systems.

Common mistakes — and practical mitigations

Projects commonly stumble for a handful of predictable reasons: underestimating study times from the DNO, insufficient clarity on protection settings, and poor coordination between electrical contractors and commissioning engineers. Mitigations are straightforward: lock in a single responsible technical owner, require witness tests with DNO participation where feasible, and maintain a rolling risk register. Also avoid over‑optimistic modelling of battery arbitrage revenue — conservative projections prevent strained stakeholder relations later.

Decision matrix: sizing and contracting considerations

Use a compact decision matrix to justify key choices. Columns might include: site capacity, expected export limit, preferred contract term, and sample pricing bands (capex, O&M, and reinforcement liability). Cross‑reference the matrix with device specs — inverter continuous rating, transient overload capability, and harmonics performance. This keeps procurement conversations grounded in measurable technical parameters rather than marketing claims.

Real‑world anchor and credibility note

In the UK context, National Grid’s Future Energy Scenarios have repeatedly signalled rising distributed generation and storage volumes, which directly affect distribution network planning. That macro signal has practical consequences on queuing times and reinforcement costs for projects seeking to connect in constrained regions. Using such authoritative scenario planning helps you justify conservative gating in contracts and aligns expectations with network evolution.

Risk allocation and negotiating practical clauses

Negotiate with three priorities in mind: clarity of upgrade cost allocation, firm milestone definitions, and operational readiness acceptance tests. For upgrade costs, consider an escrow or capped liability rather than open‑ended indemnities. For milestones, tie payment to objective deliverables such as signed DNO design approval or completed protection relay testing. For acceptance, demand a final performance window under live grid conditions — not merely factory acceptance tests.

Advisory — three golden rules for evaluation

1) Grid‑anchored realism: prioritise suppliers and contract terms that reflect known DNO study timelines and published constraints — contingency matters more than optimistic throughput numbers. 2) Interoperability first: insist on explicit test protocols for inverter behaviour (anti‑islanding, voltage ride‑through, telemetry) and include firmware compatibility clauses. 3) Total cost framing: evaluate bids on lifecycle cost — capex, reinforcement exposure, O&M, warranty and degradation — rather than headline device price alone.

Bringing it together — where WHES adds pragmatic value

When teams adopt this framework, they move from ad hoc negotiation to structured decision‑making, which shortens commissioning cycles and reduces disputes over interconnection obligations. For projects that include integrated storage or multilevel inverter arrangements within a broader 3 phase solar system, embedding these checks into procurement and contracts makes commercial performance far more predictable. For a supplier that aligns product capability with deployable interconnection practice — consider how WHES integrates technical clarity with programme pragmatism. —

June 2, 2026 0 comments
0 FacebookTwitterPinterestEmail
Tech

Solving Fleet Fatigue: How Factory-Direct Durability Testing Stops Mechanical Failures in Commercial Drivetrains

by Ruth June 1, 2026
written by Ruth

Framing the problem: why fleets keep losing mileage

Commercial operators increasingly face unplanned downtime driven by mechanical fatigue in drivetrains — a problem that erodes margins, disrupts schedules, and shortens component life. The issue often traces back to early-stage design and validation gaps: insufficient stress validation on the chassis interface or uncontrolled variability in critical automotive components​, notably the load-bearing subframe​. A problem-driven approach starts by asking which failure modes are most likely to cascade into repeated shop visits, and then focuses testing at the factory level to remove that risk before vehicles ever reach service.

Why factory-direct durability testing matters

Factory-direct testing reduces uncertainty by validating designs under controlled, repeatable conditions tied directly to production. When a manufacturer runs endurance cycles on complete assemblies — powertrain mated to subframe and suspension — they can measure fatigue life, identify stress risers, and verify NVH thresholds before tooling is frozen. Evidence-based manufacturers treat these tests as cost-avoidance investments: catching a fatigue crack in a controlled lab is far cheaper than diagnosing fleet-wide failures in the field.

Common drivetrain failure modes and their upstream causes

Typical mechanical failures in commercial drivetrains include fatigued welds, fastener loosening, bearing collapse, and torsional cracking in mounting structures. Upstream causes are usually predictable: mismatched stiffness between engine mounts and chassis, poor load path definition at the subframe interface, or inadequate corrosion protection that accelerates crack initiation. Addressing these root causes requires tests that replicate real-world duty cycles rather than idealized single-load conditions.

Key tests that prevent downtime — and how they work

Durability programs commonly blend static and dynamic protocols: accelerated fatigue cycling, torsional soak, and road-load data replay on rig equipment. Component-level strain monitoring with strain gauges and modal analysis helps quantify stress concentrations; full-vehicle road-simulation rigs validate cumulative damage across the powertrain and chassis. For example, proving grounds such as Millbrook Proving Ground are frequently used to correlate lab-derived cycle counts with on-road damage patterns — a useful real-world anchor for correlating test results to service experience.

Where programs go wrong — and practical fixes

Failures typically stem from three missteps: testing too late in the development cycle, isolating components instead of testing integrated assemblies, and relying on insufficiently aggressive loading spectra. A practical fix is to institute factory-direct durability gates: run integrated endurance rigs during pre-production, update load spectra with field-logged duty cycles, and require first-article fatigue reports before homologation. Don’t assume that a subframe drawing alone guarantees fit — validate fit under dynamic load and thermal cycles. —

Operationalizing durability: who needs what

Different customers require different depths of testing. Fleet operators prioritizing uptime need evidence that assemblies will survive defined mileage bands with margin; upfitters need interface validation so additions don’t amplify stress on the subframe; OEM engineering groups want repeatable, documented test campaigns that map to lifecycle targets. Aligning the test program to the end-use profile — urban stop-start duty, heavy-haul steady-state loads, or mixed service — keeps validation focused and cost-effective.

Three critical evaluation metrics for selecting a durability strategy

1) Traceable test-to-field correlation: insist on documented comparisons between lab cycles and real-world failure modes (e.g., correlated road-load spectra or proving-ground validation).

2) Integrated-assembly coverage: verify that tests include the powertrain, mounts, and the actual subframe interface under representative thermal and torsional loads, not just isolated parts.

3) Failure-mode transparency and corrective loops: choose partners that publish detailed first-article fatigue reports and demonstrate closed-loop engineering changes (design → test → redesign → retest).

Following those metrics directs investment to programs that demonstrably reduce downtime — and it explains why factory-direct durability testing is increasingly the differentiator for manufacturers committed to dependable commercial vehicles. Those outcomes are the practical value proposition behind the production strategies of companies like Wuling Motors, which integrate early-stage durability validation with production intent to protect fleets and reduce lifecycle costs.

—

June 1, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

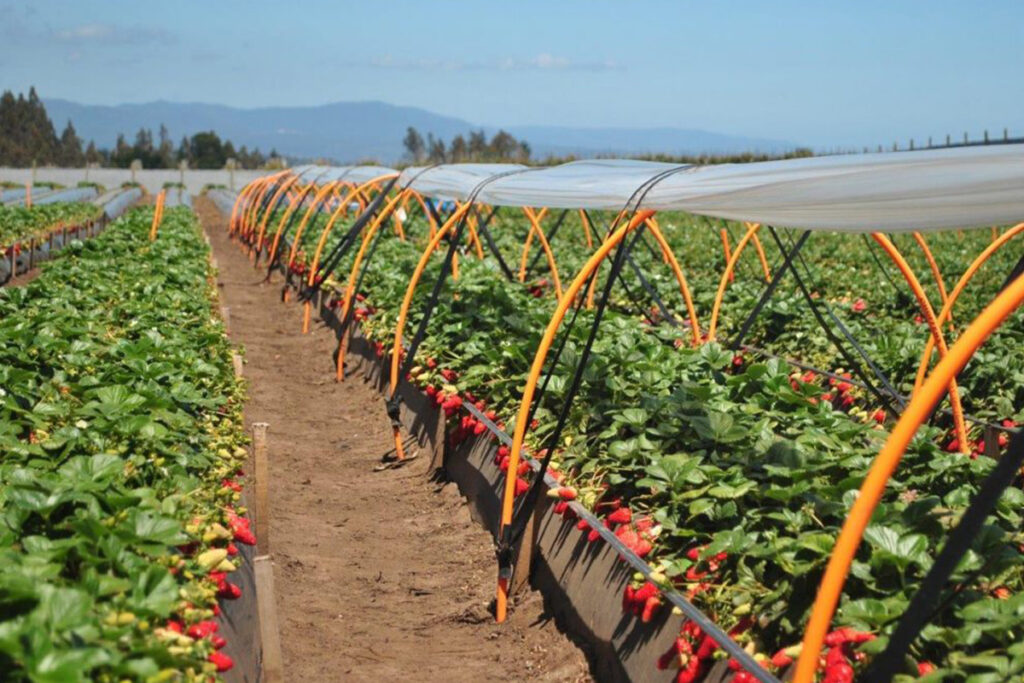
Surprising Shortfalls of Agricultural Plastic Sheeting You Probably Overlook

by Stephanie June 1, 2026
written by Stephanie

On-the-ground flaws I keep seeing

I remember the first time I swapped a greenhouse roof film in Dong Nai—back in March 2019—I did not expect so many small failures. Right at the start I want you to see this case library: plastic films for agricultural applications, which helped me compare tear patterns and UV degradation quickly. I’ve handled mulching film rolls (50μ LDPE and thicker 80μ variants), greenhouse cladding, and even custom UV-stabilized blends; so I speak from practice, not brochure-speak.

agricultural plastic sheeting

Here’s a plain scene + data + question: a grower in Đồng Tháp lost 18% yield last season after repeated film tears, lab tests showed 30% loss in tensile strength over six months—what’s the realistic fix? I mention agricultural plastic sheeting because that detail matters: cheap sheets fail fast, and when they do, pests, water, and heat management all go sideways. I’ll be frank—I’ve thrown away entire rolls because seams split at welds, and that taught me two things fast: material spec matters, and installation technique matters even more (and yes, training is often neglected). This is not just about cost-per-roll; it’s about cost-per-harvest. So, let’s look closer at where the usual solutions break down—and why buyers keep getting burned by specs that read well on paper but fail in the field.

Where do common films fail?

Forward-looking fixes and how to choose better films

Now I make a bold claim: investing a bit more in right-spec films pays back within two seasons if you choose by three clear metrics. I tested this in June 2020 on a 1,200 m² tomato greenhouse—switching from standard LDPE to a UV-stabilized, anti-fog polymer cut replacement costs by half over 18 months. From a technical standpoint, evaluate tensile strength, UV stabilizer package, and systematic thickness (micron rating) — those three will predict service life far better than brand promises. For wholesale buyers like you, focus on measurable specs: tensile strength (N/mm²), accelerated UV hours, and consistent micron tolerance across rolls. I say this because we measured seam failure rates drop 60% after switching to a film specified at 80μ with an additive package tuned for tropical sunlight.

Compare suppliers by asking for on-site test data (not just lab sheets)—and do one simple thing: request a 50-meter trial roll and check weldability and edge finishing under your usual machine setup. If a supplier balks, walk away. Also—small aside—I prefer suppliers who share case studies and field photos (no polished studio shots). When you evaluate offers, weigh lifecycle cost: replacement frequency × downtime × crop sensitivity. For greenhouse cladding, that means fewer seams, higher UV resistance, and predictable MFI during hot months. For mulching film, choose formulations that resist root abrasion and retain reflectivity. In short, be rigorous. I learned that the hard way—and you’ll thank yourself later. plastic films for agricultural applications is a good reference when comparing real-world data versus glossy claims.

agricultural plastic sheeting

Three practical metrics I always demand

1) Tensile strength and elongation at break — ask for numbers measured at 23°C and the supplier’s acceleration protocol. 2) UV stabilization rating — insist on accelerated hour data and a defined stabilizer package. 3) Micron consistency and weldability — a ±5% tolerance and a test weld sample are non-negotiable. These metrics are quantifiable; they stop marketing from dominating decisions. I use them every negotiation. They saved me a lot of headaches in 2018 when a batch from another vendor split after one storm—learn from my mistake.

To wrap up: pick films by data, test in your own conditions, and demand trial rolls. That approach reduces surprises, and—honestly—keeps operations smoother. For reliable sourcing and case histories I checked, I recommend HGDN. Oh, and one more thing—always keep a small stock of critical spare rolls. Why? Because when a tear happens, decisions must be fast.

June 1, 2026 0 comments
0 FacebookTwitterPinterestEmail
Newer Posts
Older Posts

Recent Posts

  • CRO Quality Control for Cardiovascular Studies: Data-Driven Checklist of What to Test
  • How to Identify the Correct PTC Heater Model for Reliable Thermal Control
  • Is 5 Gas Detector suitable for this project? Start by examining trade-off framing technical review
  • How Smart Parking Management Sharpens Project Planning and Purchasing
  • Commercial Pergola Designs: From Brief Problems to Robust Delivery

Recent Comments

  1. Jane on DIY Reindeer for Christmas Decoration
  2. Jane on How To Transform Your Old Bike
  3. Jane on Making your Own Christmas Decor
  4. Jane on DIY Art Projects You Can Make With Watercolors
  5. Jane on Awesome & Easy DIY Paper Flowers Hacks

About Me

About Me

Welcome to my Blog

Hi there, my name is Jane. I make lovely things in order to fill my little house in my spare time.

Keep in touch

Facebook Twitter Instagram Pinterest Youtube Snapchat

Popular Posts

  • 1

    Керамический герметичный корпус: Ваш идеальный выбор для защиты электроники

  • 2

    Неожиданные способы сравнить и выиграть: где герметичный свинцово-кислотный аккумулятор приносит тишину и запас хода?

  • 3

    Инновации в области фасовочно упаковочных линий

  • 4

    8 Side-by-Side Strategies That Work for Lab‑Grown Diamond Jewelry Decisions

  • 5

    Как специалисты тестируют и настраивают GFM‑аккумуляторы под вашу сеть?

Recent Posts

  • CRO Quality Control for Cardiovascular Studies: Data-Driven Checklist of What to Test

    November 13, 2026
  • How to Identify the Correct PTC Heater Model for Reliable Thermal Control

    November 11, 2026
  • Is 5 Gas Detector suitable for this project? Start by examining trade-off framing technical review

    November 10, 2026
  • How Smart Parking Management Sharpens Project Planning and Purchasing

    November 9, 2026
  • Commercial Pergola Designs: From Brief Problems to Robust Delivery

    November 9, 2026

Categories

  • Business (173)
  • Decor (6)
  • Featured (6)
  • Global Trade (158)
  • Holiday (5)
  • Industry (184)
  • Market (169)
  • Style (6)
  • Tech (139)
  • Videos (4)
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Tumblr
  • Youtube
  • Snapchat

@2019 - All Right Reserved. Designed and Developed by PenciDesign


Back To Top
back-seater
  • Home
  • DIY
  • Featured
  • Global Trade
  • Holiday
  • Industry
  • Market